Commercial Bakeware Quality
Commercial Bakeware Dimensional Inspection: Datums, Gauges and Acceptance Criteria
A B2B buyer guide to translating commercial bakeware drawings into repeatable inspection methods, sampling rules and supplier acceptance evidence.
Start with function, not a long list of dimensions
Separate characteristics that control equipment fit, product geometry, stacking, lid engagement and safe handling from dimensions that only describe the part. A purchase drawing should make the critical-to-function features visible so inspection effort follows operational risk.
Define whether each requirement applies to a single cavity, the assembled pan or tray, a strapped set, a stack or a rack-loaded condition. State the inspection state as received, after coating, after conditioning or after a specified bake-and-wash cycle.
Match the gauge to the characteristic
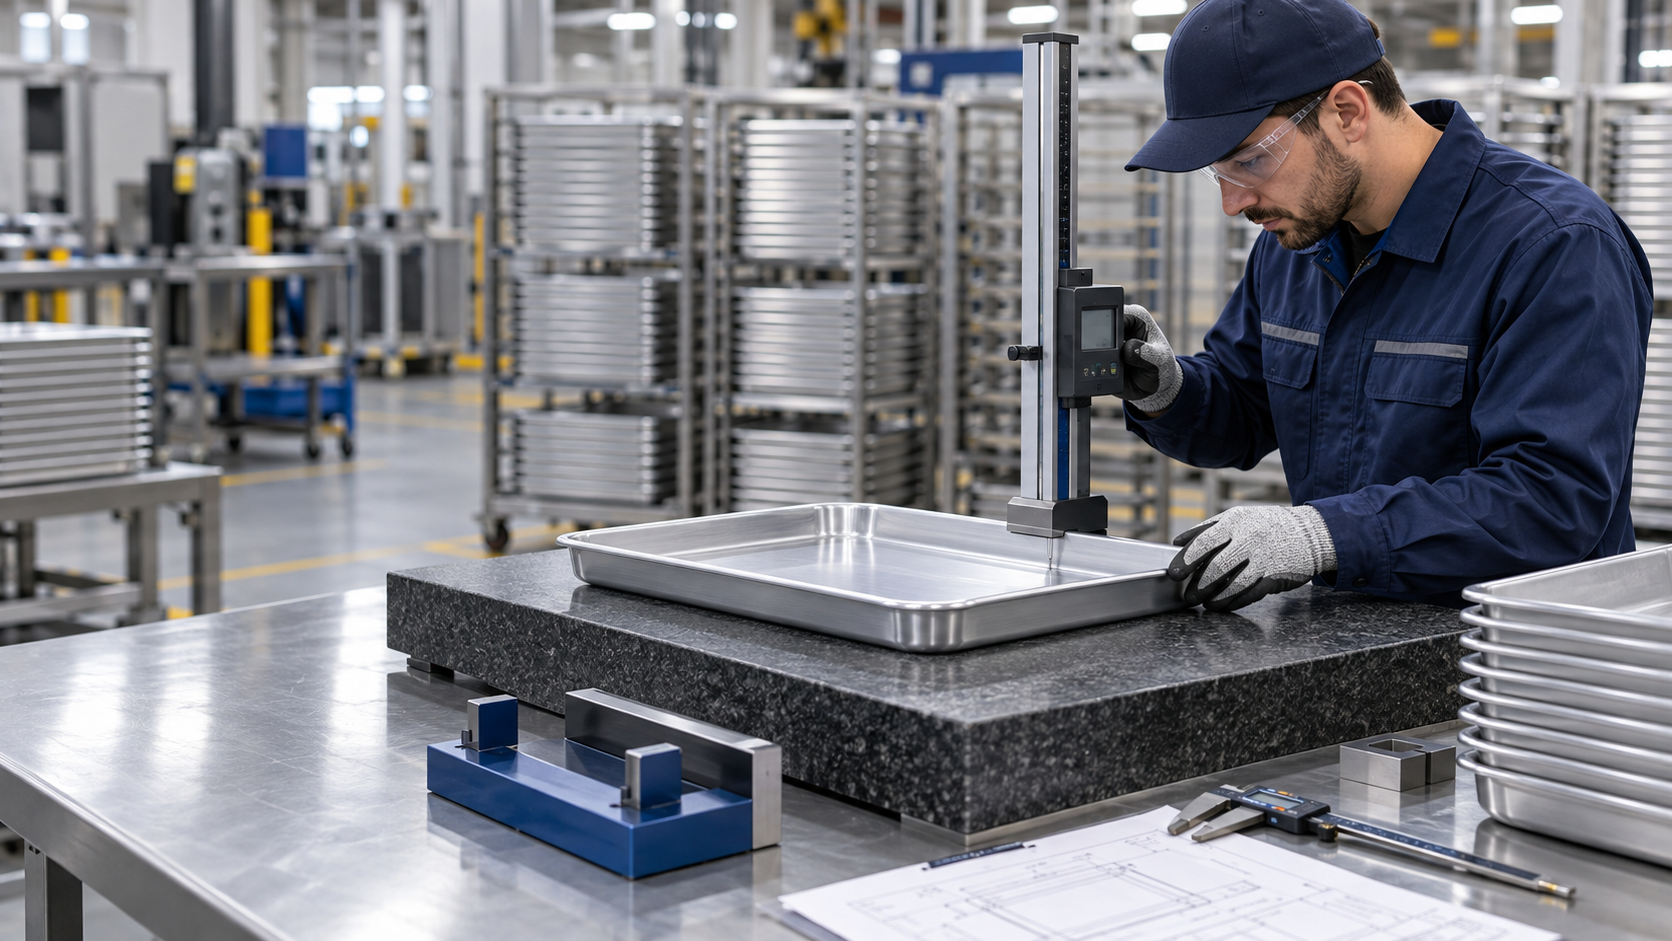
Use calipers or micrometers for accessible sizes, height gauges for flange and depth relationships, surface plates and indicators for controlled form checks, pins or plug gauges for holes, and functional fixtures for interfaces that must mate with conveyors, lids or racks.
A gauge should resolve the tolerance comfortably, contact the intended surface without damaging a coating and be practical at the required sampling rate. Record the instrument ID, calibration status, measurement range and method revision with the result.
Verify the measurement process before trusting the data
Run a repeatability and reproducibility study on the actual characteristic, part geometry, fixture and operators. NIST describes gauge studies around artifacts, operators, gauges and configurations, with attention to repeatability, reproducibility, stability, bias, resolution, linearity, hysteresis and drift.
If measurement variation consumes too much of the product tolerance, improve the fixture, method, training or gauge before tightening the pan specification. Otherwise inspection noise can create false rejects, false accepts and supplier disputes.
Define sampling by lot, risk and process evidence
State what forms a lot, how units are selected, which characteristics receive 100 percent inspection and which use sampling. New tooling, repaired tooling, coating changes, process moves and corrective actions should trigger increased verification until capability is re-established.
For multi-cavity or strapped products, sample positions as well as assemblies. Edge and center cavities, first and last stations, and multiple orientations can reveal systematic forming or joining variation hidden by one convenient measurement point.
Use drawings and reports that prevent interpretation gaps
ASME Y14.5 provides a standardized language for communicating design intent, datums and geometric controls. Buyers can reference the agreed edition when appropriate, but every requirement still needs a clear value, feature scope and inspection method understood by both parties.
The report should include drawing and method revision, lot identity, sample size, actual values, units, acceptance decision, nonconformance disposition and traceable instrument records. Photographs or fixture sketches help preserve the setup for future lots.
Close acceptance with correlation and change control
Before mass production, have buyer and supplier measure the same production-intent samples and reconcile differences. Correlation is especially important for flatness, twist, diagonal, profile, cavity pitch and coated surfaces where setup choices materially change the result.
Freeze the approved drawing, datum scheme, fixture, gauge program, sampling plan and report format. Require written approval before changing forming tools, joining sequence, coating build, fixture logic or inspection software that can alter measured conformance.
Dimensional Inspection Method Matrix
| Characteristic | Suggested method | Method details to freeze |
|---|---|---|
| Overall envelope | Caliper, height gauge or functional frame | Datums, contact points and coated condition |
| Cavity pitch and location | Height gauge, CMM or dedicated fixture | Feature centers, datum alignment and pattern scope |
| Flange flatness or twist | Surface plate, controlled supports and indicator | Support map, loading, scan path and temperature |
| Hole or perforation size | Pin gauges, optical system or sampling fixture | Gauge class, location plan and burr treatment |
| Lid, rack or conveyor fit | Production-equivalent functional gauge | Insertion force, clearance, orientation and wear limits |
| Coating-affected size | Non-damaging dimensional method | Precoat versus final limits and cure condition |
Technical references: ASME Y14.5 Dimensioning and Tolerancing for the shared language of design intent and geometric controls; NIST Gauge R&R studies for characterizing production measurement processes. Apply the editions and acceptance rules agreed in the purchase specification.
Frequently Asked Questions
Which commercial bakeware dimensions should be critical?
Mark dimensions as critical when they control line fit, cavity pitch, lid engagement, stacking, product geometry, depanning, rack clearance or another defined function. Do not label every dimension critical.
Why do buyer and supplier measurements disagree?
Common causes include different datums, fixtures, support points, clamping force, temperatures, instruments, measurement locations or drawing revisions. A correlation study on the same samples usually exposes the gap.
Should coated bakeware be measured before or after coating?
State the required inspection stage for each characteristic. If coating build affects fit or cavity size, define both the manufacturing control and the final coated acceptance condition.
Is a calibration certificate enough to prove the measurement is reliable?
No. Calibration supports instrument traceability, while the full measurement process also depends on resolution, fixture, method, operator, environment and the part itself. Verify repeatability and reproducibility on the real application.
What should a bakeware dimensional report include?
Include lot and part identity, drawing revision, method revision, datum and fixture setup, instrument ID and calibration status, sample size, actual results, units, acceptance decision and any approved disposition.
Quality Planning Review
Make every critical dimension measurable and auditable.
Send the drawing, mating-equipment interfaces, critical product dimensions, coating condition, expected lot size and current inspection concerns. Bakeware China can prepare a production-intent inspection matrix and sample report for review.
For production-line heat decisions, use the commercial bakeware thermal mapping and oven profile validation guide to define sensor maps, load boundaries and acceptance criteria.
For hygienic drainage and drying criteria, use the commercial bakeware drainage and drying guide.